
Troubleshooting Sticky or Incomplete Resin 3D Prints: Common Fixes

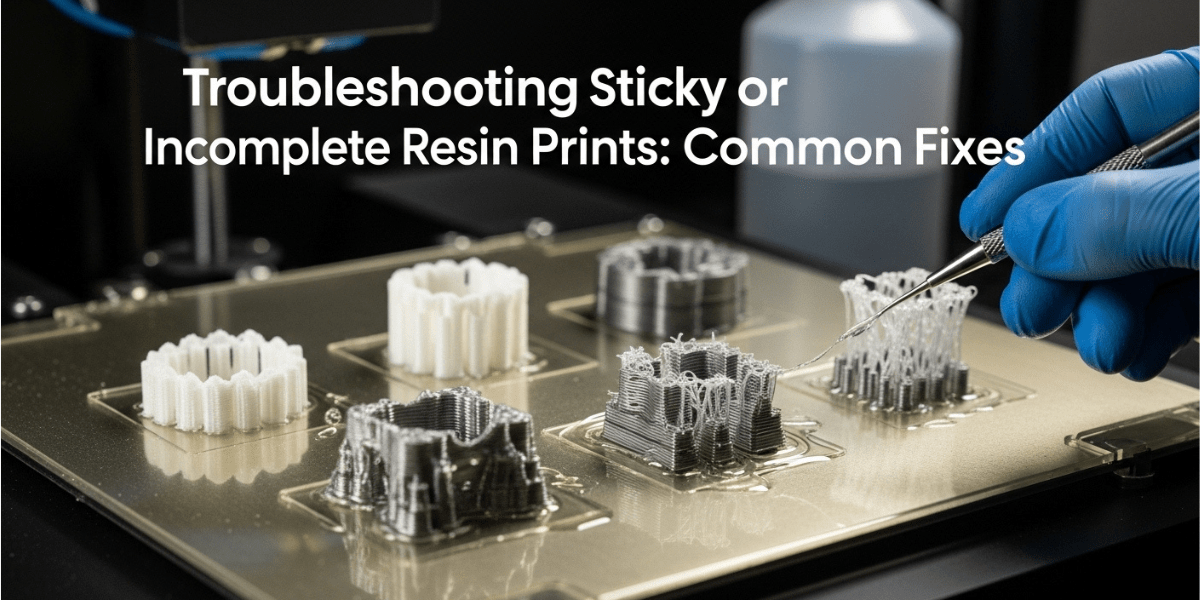
Resin 3D printing can produce highly detailed models with smooth surfaces and sharp features. However, even a well-maintained resin 3D printer can sometimes produce sticky surfaces, incomplete layers, weak supports, or failed prints.
These problems can be frustrating, especially after a long printing session. Fortunately, many resin 3D printing problems have identifiable causes and practical solutions.
In this guide, MCast explains the most common causes of sticky and incomplete resin prints. You’ll also learn how to troubleshoot resin 3D printer failures and improve your printing results.
1. Sticky Resin Prints After Washing
A print that remains sticky after washing usually has residual uncured resin on its surface. In some cases, the washing process may not have removed enough resin.
Common Causes of Sticky Prints
Sticky surfaces can result from several factors:
- Used or contaminated cleaning solvent
- Insufficient washing
- Complex model geometry
- Resin trapped inside cavities
- Incorrect post-processing
- Resin-specific curing characteristics
Formlabs recommends using clean solvent and multiple washing stages when necessary. This can help remove residual resin from printed surfaces.
How to Fix Sticky Resin Prints
Try these steps:
- Use fresh IPA or the cleaning solution recommended for your resin.
- Increase washing time for complex models.
- Use a soft brush for difficult areas when appropriate.
- Allow the print to dry completely after washing.
- Follow the resin manufacturer’s recommended curing process.
Avoid assuming that every resin requires the same curing time. Always check the manufacturer’s instructions.
2. Incomplete Layers or Missing Details
Incomplete prints can appear as missing sections, weak walls, gaps, or partially formed models.
These problems often indicate insufficient curing or mechanical issues during printing.
Check Your Exposure Settings
Exposure time controls how much UV energy reaches each resin layer.
If exposure is too low, layers may not cure sufficiently.
Run an Exposure Test
Instead of making large changes immediately, use a suitable exposure test model.
Adjust the exposure according to the resin and printer manufacturer’s recommendations.
Different resins can require different exposure settings.
Check the Resin Vat and FEP Film
A dirty or damaged resin vat can contribute to printing problems.
Inspect the FEP or release film for:
- Cloudiness
- Scratches
- Damage
- Cured resin
- Contamination
A damaged or contaminated film can interfere with reliable layer separation.
Mix the Resin Properly
Resin can separate during storage.
Shake the bottle according to the manufacturer’s recommendations before pouring it into the vat.
If required, gently mix the resin in the vat before starting another print.
3. Resin Prints Separating From the Build Plate
One of the most common resin 3D printer problems is poor build-plate adhesion.
The first layers need enough adhesion to remain attached while each new layer is peeled from the release film.
Check the Build Plate Level
An incorrectly leveled build plate can prevent proper contact during the first layers.
Re-Level the Build Plate
Follow your printer manufacturer’s leveling procedure.
Also make sure the build plate is securely tightened before starting a print.
Adjust Bottom Exposure
Bottom exposure is normally higher than regular exposure.
This gives the initial layers stronger adhesion to the build plate.
If the print continues failing, increase bottom exposure gradually rather than making large changes.
Check Your Bottom Layers
The number of bottom layers also affects initial adhesion.
If your settings are unsuitable for the resin, the print may detach from the platform.
Use the resin manufacturer’s recommended profile as your starting point.
Consider Resin Temperature
Cold resin can become more viscous and may behave differently during printing.
Keeping the printer and resin within the manufacturer’s recommended operating range can improve consistency.
4. Prints Failing Halfway Through the Job
A print that starts successfully but fails later has a different problem from a print that never adheres.
Check Your Supports
Weak or poorly positioned supports can cause the model to separate during printing.
Improve Support Placement
Add stronger supports to areas carrying significant weight.
Avoid placing supports randomly across important surfaces.
The model’s orientation also affects the forces acting on the supports.
Check Lift Speed
Each printed layer must separate from the release film.
Excessive lifting speed can increase separation forces.
If supports repeatedly fail, reducing lift speed can help lower these forces.
Check Large Flat Surfaces
Large cross-sections can create greater peel forces during printing.
Changing the model orientation can reduce the area exposed to each layer.
This can make the printing process more stable.
5. Overexposed or Underexposed Resin Prints
Exposure settings affect both print quality and dimensional accuracy.
Signs of Underexposure
Underexposure can cause:
- Weak layer bonding
- Missing details
- Failed supports
- Incomplete models
- Poor build-plate adhesion
Signs of Overexposure
Overexposure can cause:
- Loss of fine details
- Enlarged features
- Blocked openings
- Excessively strong supports
- Difficult support removal
How to Find the Right Exposure
Use an exposure calibration model designed for your printer and resin.
Change one setting at a time and compare the results.
This makes it easier to identify the setting that improves print quality.
Avoid copying exposure settings from another resin without verification.
6. Uncured Resin Trapped Inside Detailed Models
Complex models can contain small cavities and recessed areas where liquid resin becomes trapped.
This is especially common with hollow prints.
Improve Drainage
Hollow models should be designed with suitable drain holes.
Why Drain Holes Matter
Drain holes allow uncured resin to escape from internal cavities.
They can also help reduce trapped resin and unwanted pressure during printing.
Clean Difficult Areas Carefully
Use an appropriate cleaning method for the resin.
A soft brush can help reach recessed areas without damaging delicate surfaces.
Inspect the model carefully before curing.
Rotate the Model During Curing
Rotating the print can help expose different surfaces to the curing light.
However, always follow the curing procedure recommended for your specific resin.
7. Resin Prints With Cracks or Layer Separation
Cracks and visible separation between layers can indicate problems with exposure, supports, orientation, or printing conditions.
Check Your Model Orientation
Poor orientation can increase stress during the printing process.
Reduce Printing Stress
Try changing the model angle to reduce large cross-sectional areas.
Review support placement around heavy or unsupported sections.
Check the Resin and Printer Conditions
Resin properties can change with temperature and storage conditions.
Make sure the resin is stored correctly and remains within its recommended operating conditions.
Also inspect the vat and release film before starting another print.
8. Common Resin 3D Printing Mistakes to Avoid
Many printing failures come from small maintenance or setup problems.
Skipping Printer Calibration
An incorrectly leveled build plate can cause poor adhesion.
Check calibration whenever the printer requires it.
Using Old or Contaminated Resin
Resin should be stored according to the manufacturer’s recommendations.
Filter resin when appropriate after a failed print.
Never leave cured debris in the resin vat.
Changing Multiple Settings at Once
Changing exposure, supports, lift speed, and layer settings together makes troubleshooting difficult.
Instead, change one variable at a time.
This makes it easier to identify the actual cause.
Ignoring the Resin Manufacturer’s Profile
Every resin can behave differently.
Use the manufacturer’s recommended settings as your starting point.
Then calibrate them for your specific printer when necessary.
Resin 3D Printer Troubleshooting Checklist
Before starting another print, quickly check the following:
- Is the build plate correctly leveled?
- Is the build plate clean?
- Is the resin properly mixed?
- Is the resin within its recommended temperature range?
- Are the exposure settings appropriate?
- Is the resin vat clean?
- Is the FEP or release film undamaged?
- Are the supports strong enough?
- Is the model orientation suitable?
- Are hollow models properly drained?
- Are washing and curing procedures correct?
Working through this checklist can help identify common resin printing failures before they waste another print cycle.
Final Thoughts
Sticky surfaces, missing layers, poor adhesion, and failed models are common challenges in resin 3D printing. However, most problems become easier to solve when you identify the failure before changing your settings.
Start with basic checks such as cleaning, leveling, resin condition, and exposure settings.
Then examine supports, model orientation, lift speed, and post-processing.
Most importantly, use the recommended settings for your specific resin 3D printer and resin combination.
With proper calibration, regular maintenance, and a consistent workflow, you can significantly improve print reliability and achieve cleaner, more detailed resin models.
If you’re looking for resin 3D printers, resins, and printing equipment in Pakistan, you can explore the range available from MCast 3D.